


Experimental study and mechanism analysis of material damage and tool wear in CFRP variable feed drilling
-
摘要: 以T-300碳纤维/环氧树脂复合材料为研究对象,通过实验探究变进给钻削过程中损伤机理及表面质量优化方法。变进给钻削中主轴转速和最终进给速度的增大会加剧刀具磨损;刀具顶角从118°增大至135°时,刀具的磨损先减小后增大,预留进给距离对刀具磨损的影响不显著;提高主轴转速可改善孔口质量,刀具顶角对孔口损伤的影响规律与刀具磨损一致。与定进给钻削相比,变进给钻削可以降低19.4%的轴向力,但同时会加速刀具的磨损。Abstract: T-300 carbon fibre/epoxy resin composites were experimentally investigated to reveal the damage mechanism and surface quality optimization method in variable feed drilling. Results show that an increase in spindle speed and final feed speed aggravates tool wear. As the tool top angle increases from 118° to 135°, tool wear first decreases and then increases, whereas the reserved feed distance has no significant effect on tool wear. An increase in spindle speed improves hole quality, and the influence of tool top angle on hole damage follows the same trend as that on tool wear. Compared with fixed-feed drilling, variable-feed drilling reduces the axial force by 19.4%, but accelerates tool wear.
-
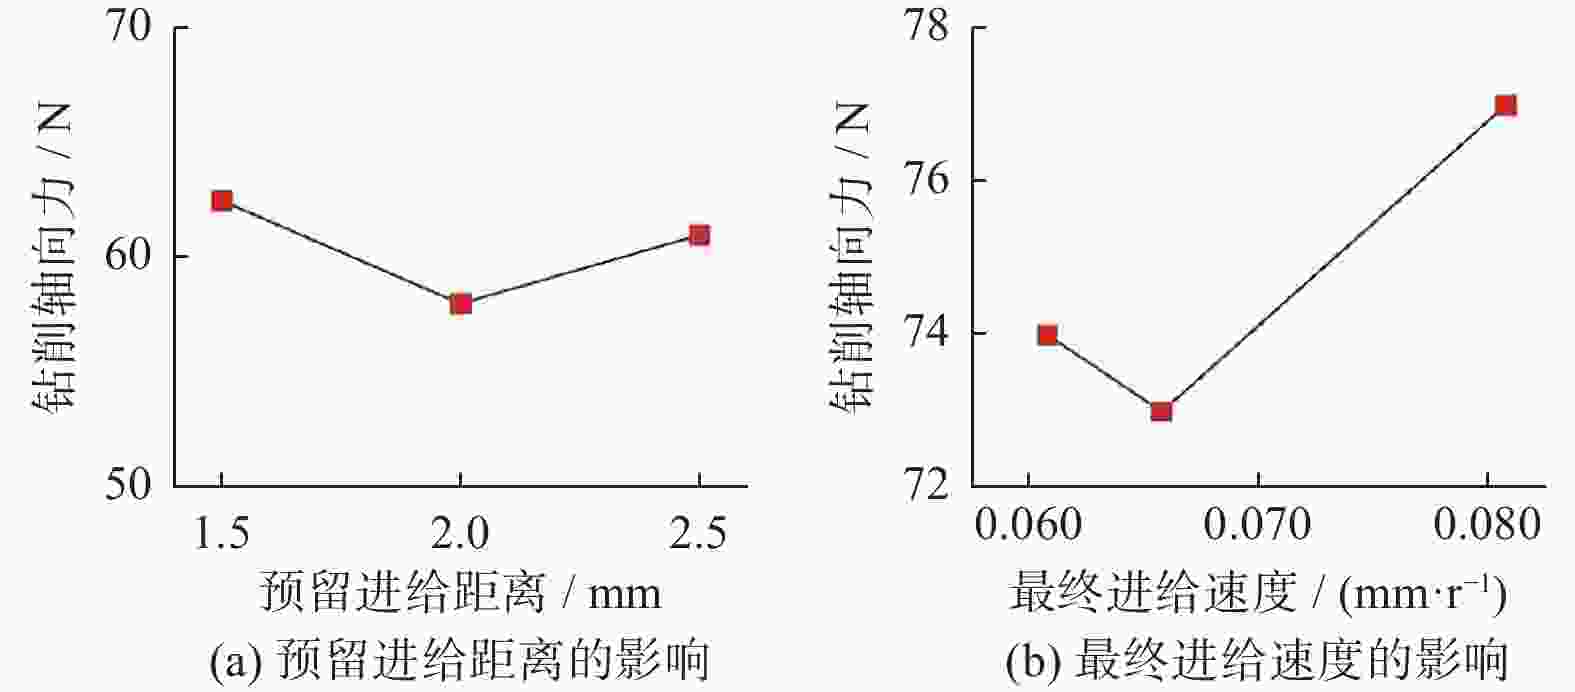
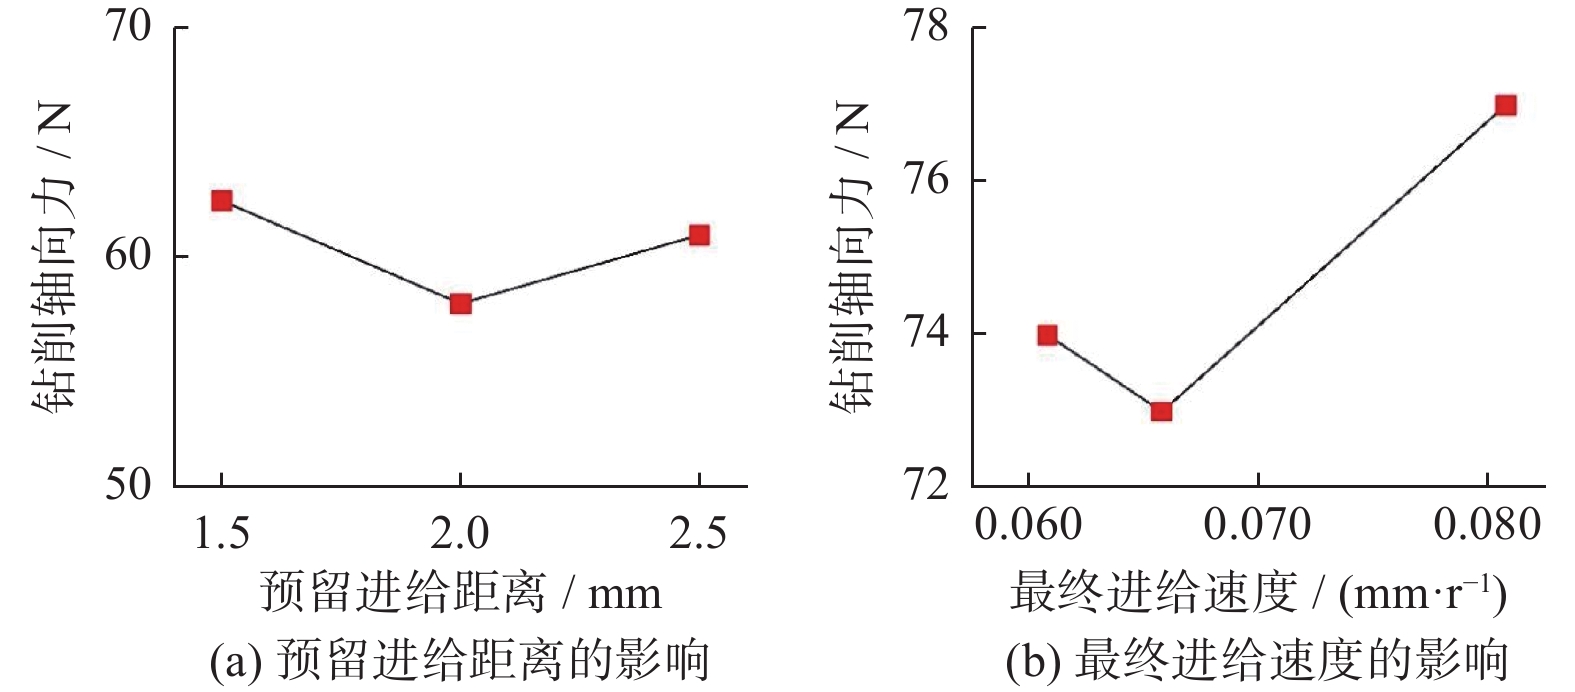
图 7 预留进给距离和最终进给速度对轴向力影响
Figure 7. Influence of reserved feed distance and final feed speed on axial force
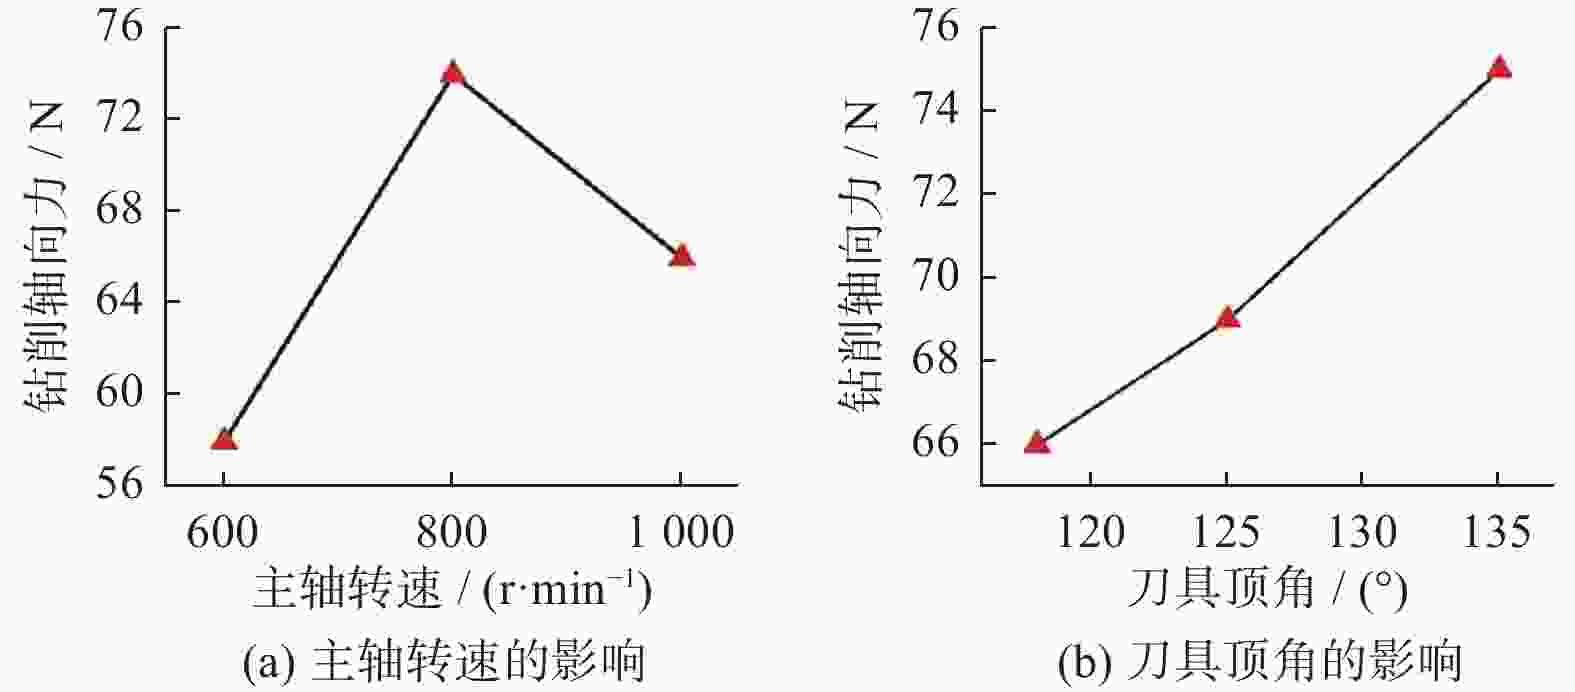
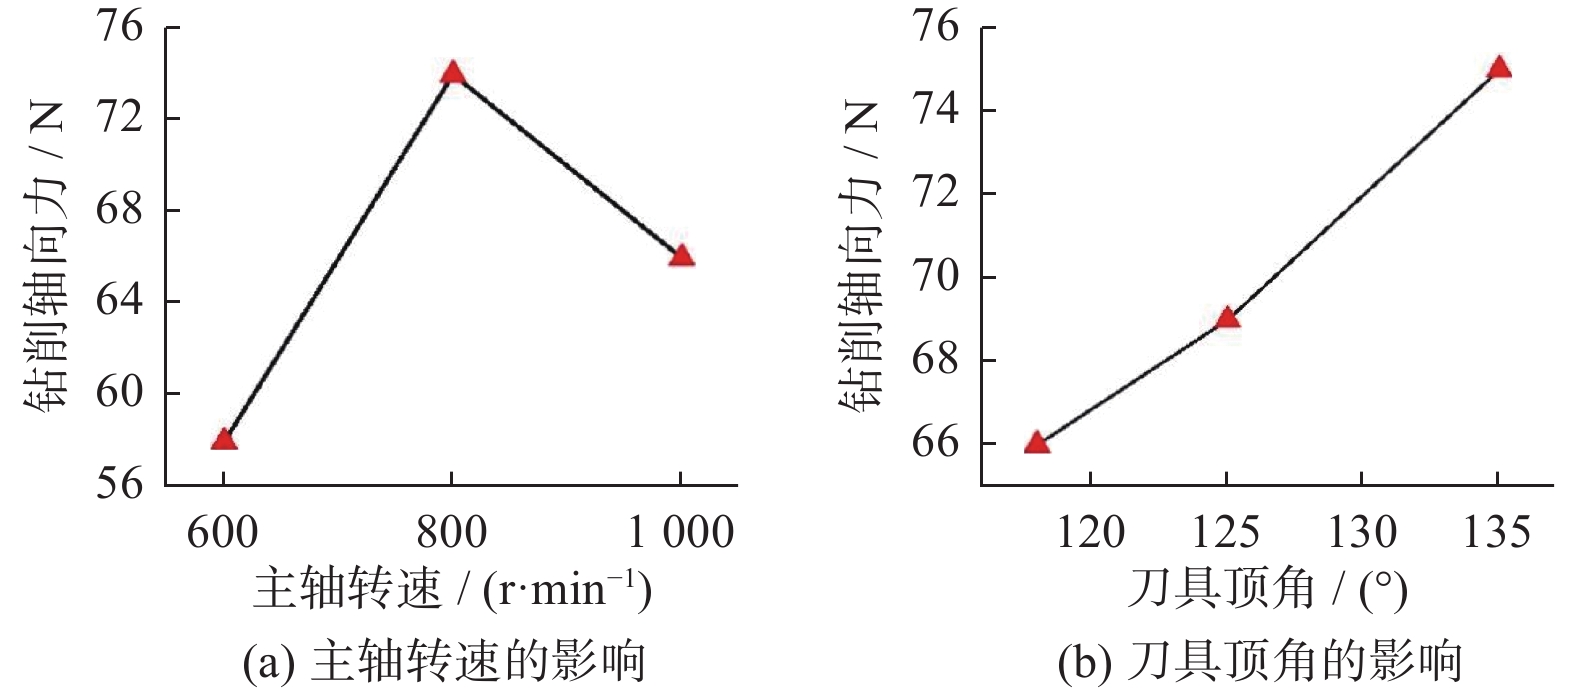
图 8 主轴转速和刀具顶角对钻削轴向力的影响
Figure 8. Influence of spindle speed and tool top angle on axial force in drilling
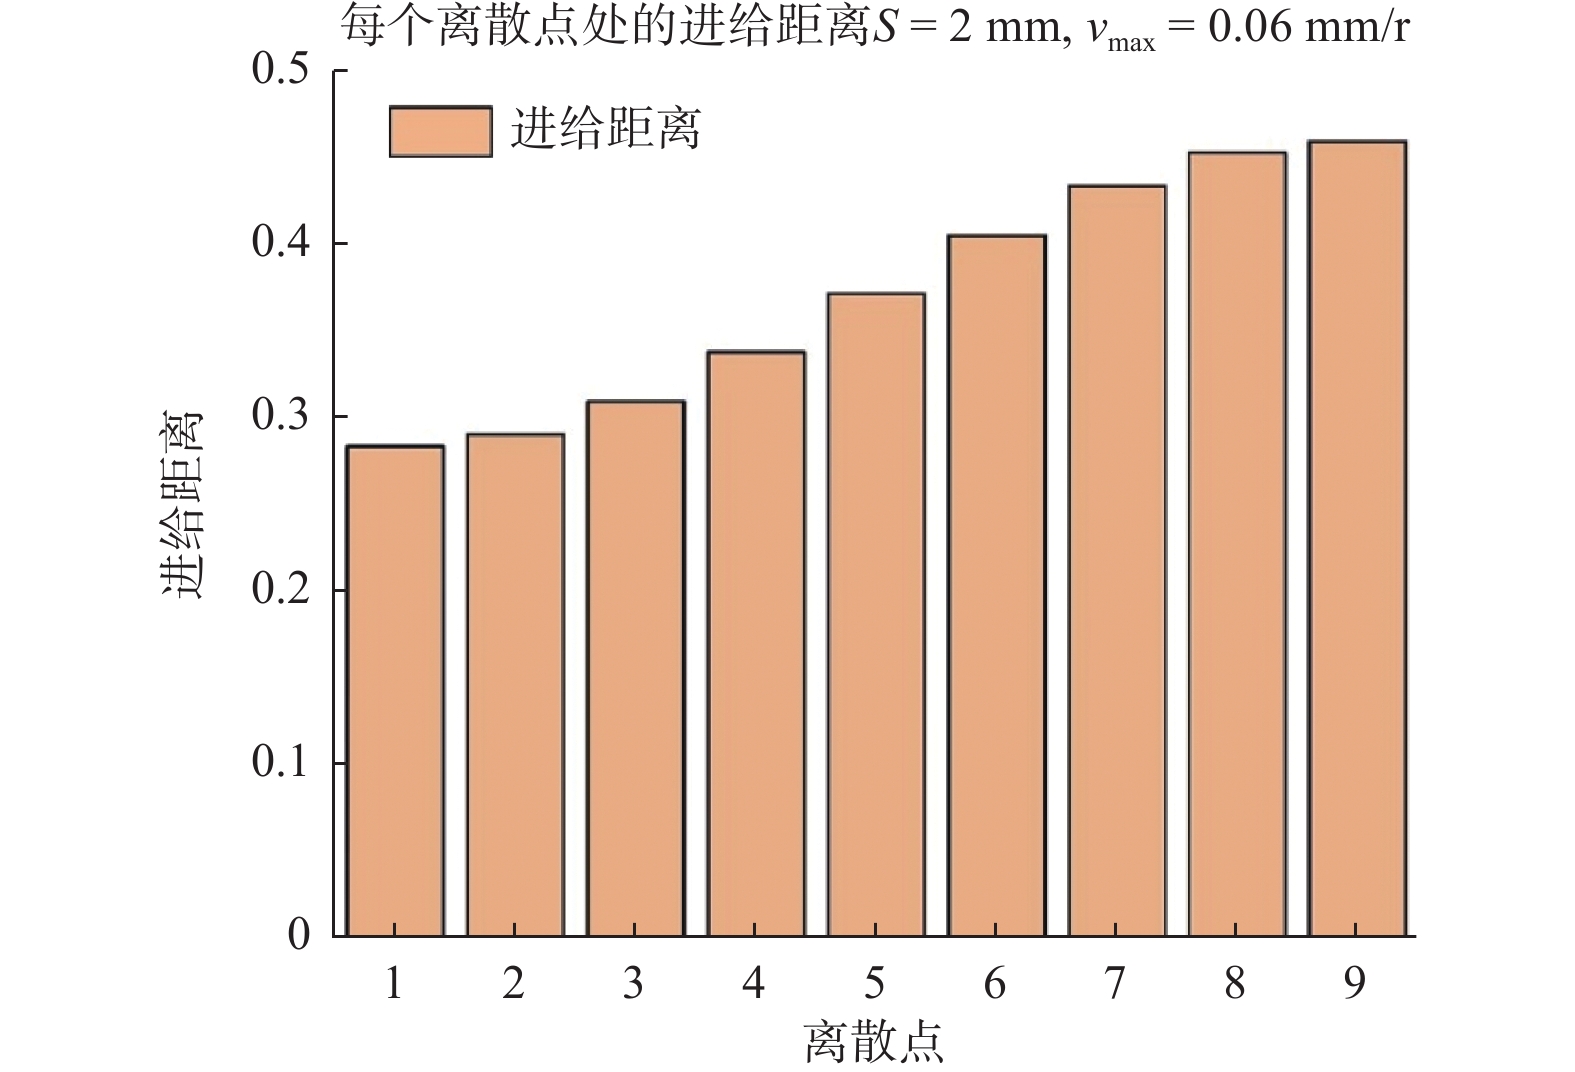
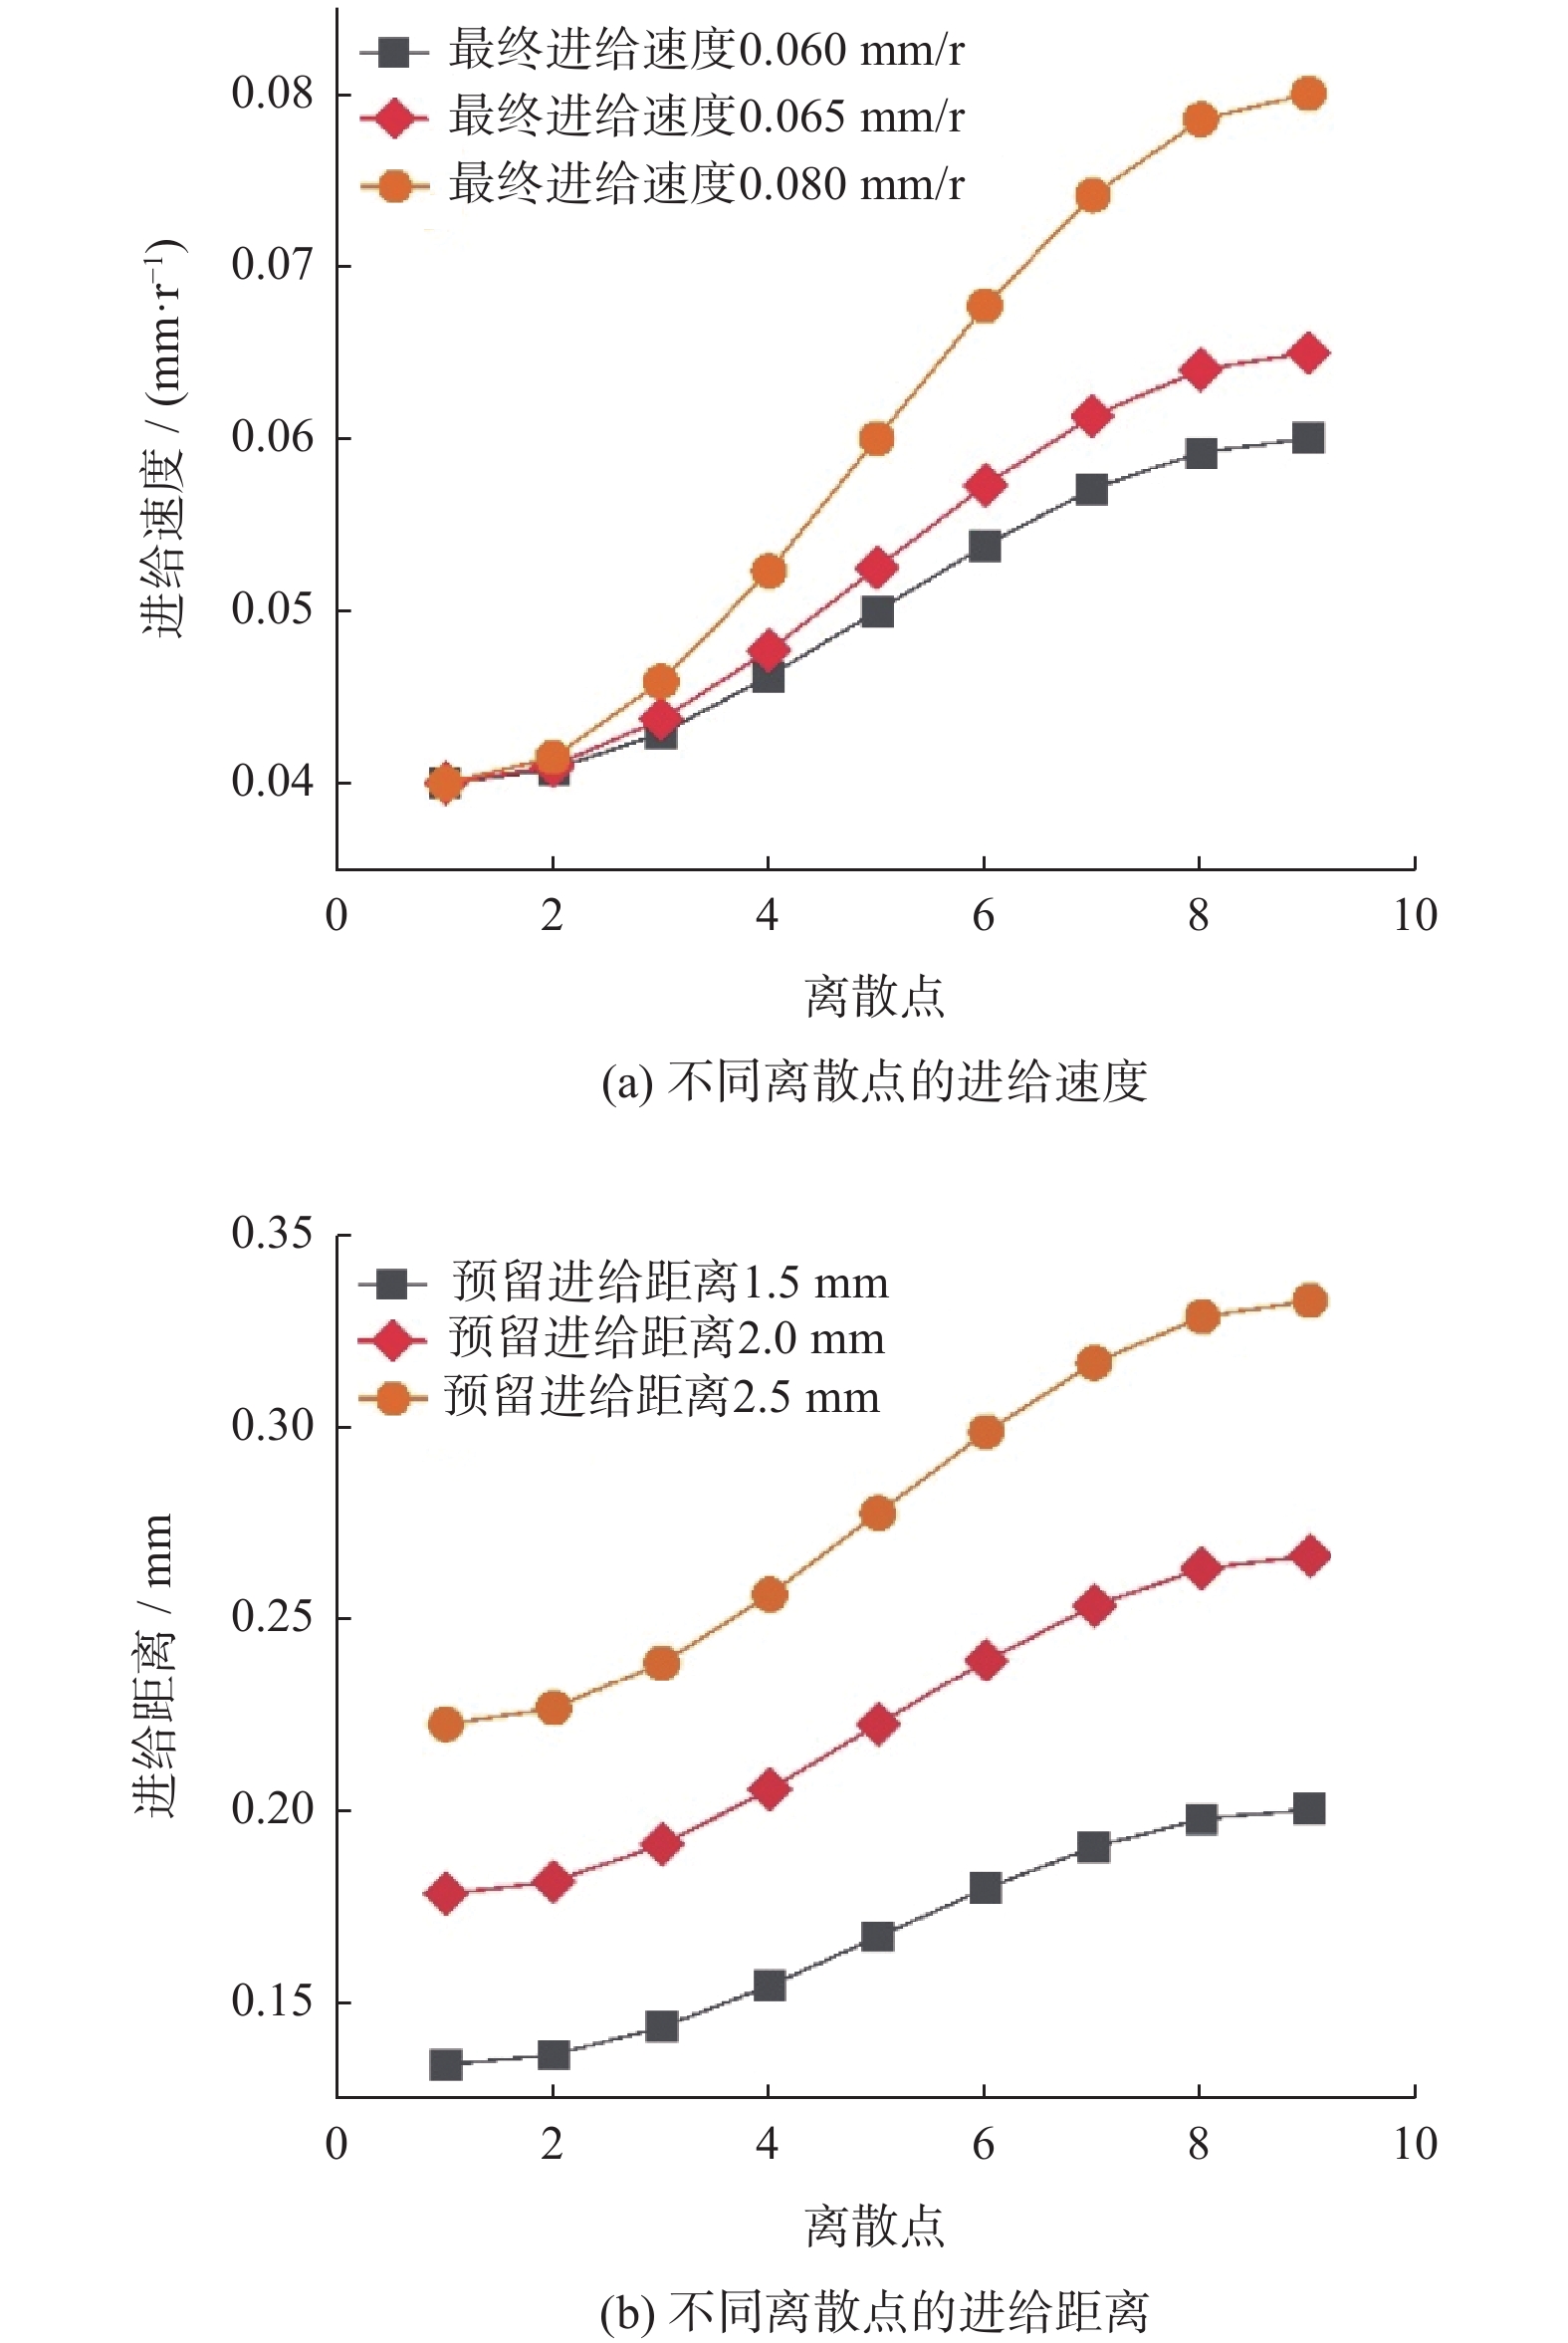
表 1 各离散点进给量分配
Table 1. Distribution of feeds at discrete points
离散点 进给距离/mm 1 0.282 2 0.289 3 0.308 4 0.337 5 0.370 6 0.404 7 0.433 8 0.452 9 0.459  下载: 导出CSV
表 2 变进给钻削实验参数表
Table 2. Variable feed drilling experiment parameter table
实验
编号主轴转速/
(r·min−1)预留的进给
距离/mm稳定区域的进给
速度/(mm·r−1)刀具顶角/
(°)1 600 2.0 0.060 118 2 800 2.0 0.060 118 3 1000 2.0 0.060 118 4 600 1.5 0.060 118 5 600 2.5 0.060 118 6 800 2.0 0.065 118 7 800 2.0 0.080 118 8 1000 2.0 0.060 120 9 1000 2.0 0.060 135
下载: 导出CSV
表 3 定进给钻削实验参数
Table 3. Experimental parameters for fixed-feed drilling
主轴转速/(r·min−1) 进给速度/(mm·r−1) 刀具顶角/(°) 600 0.054 118
下载: 导出CSV
-
[1] 康仁科, 陆冰伟, 陈凯良, 等. 超声振动辅助磨削CFRP复合材料薄管撕裂损伤研究[J] . 中国机械工程, 2024, 35(3): 524 − 533,540. doi: 10.3969/j.issn.1004-132X.2024.03.014 [2] Towsyfyan H, Biguri A, Boardman R, et al. Successes and challenges in non-destructive testing of aircraft composite structures[J] . Chinese Journal of Aeronautics, 2020, 33(3): 771 − 791. [3] Geng D X, Teng Y D, Liu Y H, et al. Experimental study on drilling load and hole quality during rotary ultrasonic helical machining of small-diameter CFRP holes[J] . Journal of Materials Processing Technology, 2019, 270: 195 − 205. [4] 曹增强. 应对我国大飞机研制的装配连接技术[J] . 航空制造技术, 2009(2): 88 − 91. [5] Geier N, Davim J P, Szalay T. Advanced cutting tools and technologies for drilling carbon fibre reinforced polymer (CFRP) composites: a review[J] . Composites Part A: Applied Science and Manufacturing, 2019, 125: 105552. [6] Gaitonde V N, Karnik S R, Rubio J C, et al. A study aimed at minimizing delamination during drilling of CFRP composites[J] . Journal of Composite Materials, 2011, 45(22): 2359 − 2368. [7] Al-wandi S, Ding S L, Mo J. An approach to evaluate delamination factor when drilling carbon fiber-reinforced plastics using different drill geometries: experiment and finite element study[J] . The International Journal of Advanced Manufacturing Technology, 2017, 93(9/10/11/12): 4043 − 4061. [8] 胡奎福, 蔡鹏, 徐春艳, 等. 碳纤维复合材料钻孔工艺与分层损伤研究[J] . 数字制造科学, 2023, 21(4): 261 − 265. [9] Mcclelland J, Murphy A, Jin Y, et al. Correlating tool wear to intact carbon fibre contacts during drilling of continuous fibre Reinforced Polymers (CFRP)[J] . Materials Today: Proceedings, 2022, 64: 1418 − 1432. [10] 徐锦泱. 碳纤维增强树脂基复合材料钻削缺陷研究进展[J] . 航空制造技术, 2022, 65(22): 24 − 33. [11] Li M J, Soo S L, Aspinwall D K, et al. Study on tool wear and workpiece surface integrity following drilling of CFRP laminates with variable feed rate strategy[J] . Procedia CIRP, 2018, 71: 407 − 412. [12] Tamura S, Matsumura T. Delamination-free drilling of carbon fiber reinforced plastic with variable feed rate[J] . Precision Engineering, 2021, 70: 70 − 76. [13] 王帅普, 梁杰, 崔松涛, 等. CFRP/Al叠层材料变进给钻削表面质量分析[J] . 组合机床与自动化加工技术, 2022(2): 95 − 98. [14] Li Y X, Jiao F, Zhang Z Q, et al. Mechanical drilling force model for longitudinal ultrasonic vibration-assisted drilling of unidirectional CFRP[J] . Journal of Materials Processing Technology, 2023, 319: 118091. [15] 吴小飞, 马保吉, 高红红, 等. 基于多目标优化的碳纤维复合材料钻削参数优化[J] . 工具技术, 2022, 56(9): 43 − 47. [16] 李东风, 王浩静, 贺福, 等. T300和T700炭纤维的结构与性能[J] . 新型碳材料, 2007, 22(1): 59 − 64. -

 下载:

 点击查看大图
计量
- 文章访问数: 10
- HTML全文浏览量: 5
- PDF下载量: 1
- 被引次数: 0
